Quick Answer: BT PCB cost is driven by material grade, BT resin content, glass style, copper, layer count, line/space, surface finish, yield risk, and supply allocation. The buyer can reduce cost only after the real driver is visible; changing suppliers without freezing the material and process assumptions usually creates a false comparison.
Key takeaways
- BT is normally more expensive than standard FR-4 because both material and package-substrate process control are more demanding.
- Layer count, line/space, ENIG or ENEPIG finish, thickness control, and reliability evidence can move the price as much as material name.
- 2026 market reports show upstream material pressure, so quote validity and material substitution rules matter.
- Cost reduction should preserve the approved material behavior, not quietly downgrade the substrate.
Table of Contents
- Why is BT PCB more expensive than standard boards?
- What are the main cost drivers?
- How much did BT material prices rise in 2026?
- How does layer count and line width affect cost?
- Why does substrate dominate advanced package cost?
- How can you reduce BT PCB cost?
- Will BT prices keep climbing?
- Bottom line: budgeting a BT project
Why is BT PCB more expensive than standard boards?
BT is more expensive because the material system and manufacturing controls are more specialized than ordinary FR-4. The substrate may need lower moisture, tighter dimensional stability, package-level surface finish, finer routing, and stronger evidence.
A buyer should not ask only ‘what is the BT price?’ The better question is: which part of the quote is material, structure, finish, yield, test, allocation, or lead-time risk?
In a cost article, start with the cost driver being priced. BT cost can come from material allocation, fine geometry, yield, finish, testing, documentation, or schedule pressure. Before comparing two quotes, the buyer needs to know which driver changed; otherwise a cheaper number may simply describe a different construction.
Cost control works only when the quote states what has been held constant. Material route, stackup, finish, test scope, and lead time should be aligned before the buyer treats unit price as a real comparison.
Cost call: A cheaper BT quote is meaningful only after the cost driver and construction are named.
The quote should also show whether cost is recurring or one-time. Tooling, engineering review, coupons, and qualification records may matter most during the first build, while material allocation, panel use, yield, and inspection time drive repeat orders. Separating those buckets helps the buyer negotiate intelligently without cutting the evidence needed for a stable production release. For a broader map of specs, applications, process limits, and sourcing questions, see the overview of BT PCB topics.
What are the main cost drivers?
| Cost driver | Why it changes price | What to ask |
|---|---|---|
| Material grade | BT content and glass style change cost | Exact grade and alternate |
| Layer count | More lamination and yield risk | Stackup and build route |
| Line/space | Fine features reduce supplier pool | Minimum and preferred rules |
| Finish | ENIG/ENEPIG adds process cost | Finish needed for package or assembly |
| Evidence | Reliability tests add time and cost | Which records are required |
Price rule: A lower price is not comparable unless all five fields match.
Another cost driver is tolerance stacking. A BT board with tight finished thickness, narrow dielectric windows, fine line/space, and strict surface finish can consume process margin quickly. The supplier may price that margin as yield risk even when the material name is unchanged. Relaxing a non-critical tolerance can sometimes reduce cost without changing the approved BT construction.
Cost evidence should show the priced assumptions: material route, layer count, line rules, finish, test scope, delivery window, and quote validity. Without those fields, a unit price is only a number, not a comparable offer.
Cost evidence should separate technical necessity from quote packaging. Material grade, glass style, layer count, line width, finish, coupons, and reliability records can each move price for a different reason. A buyer learns more from an itemized cost explanation than from a generic statement that BT is expensive.
A short quote is acceptable for a first screen, but not for cost reduction. The buyer needs the changed cost driver before approving a cheaper route.
Cost proof: Treat the price as comparable only after the quote exposes the assumptions behind the number.
How much did BT material prices rise in 2026?
As of 2026, public market reports describe broad price pressure in advanced substrate materials, especially where AI packaging demand stresses upstream resin, glass cloth, and build-up material capacity. Because exact percentages vary by supplier, contract, and region, a QueenEMS-facing RFQ should treat any public price number as market context rather than a purchase-order value.
For commercial release, request quote validity, surcharge clauses, material source, and what changes if the quoted BT construction becomes allocated. QueenEMS’ laminate price change tracker explains how to control this language.
Cost review should use material data to explain the quote, not to decorate it. Higher Tg, tighter CTE, lower moisture absorption, and controlled Dk/Df can all add cost when they require a specific grade, glass style, or qualification route.
The cost impact is rarely linear. A modest material premium may be manageable if the geometry stays inside a supplier’s normal process window. The same material can become expensive when fine line/space, tight thickness tolerance, ENEPIG, extra coupons, and short lead time arrive together. A useful cost review separates unavoidable design cost from optional documentation, schedule, or finish cost.
Use the properties to explain why cost moves. A tighter CTE requirement may force a lower-CTE grade, a lower loss target may narrow material options, and a fine-line package substrate can raise yield risk even when the resin family stays the same. The quote should price those constraints separately.
Parameter review belongs inside the cost model. Tg, Dk/Df, CTE, and moisture values can raise price when they force a specific laminate family, tighter processing, or additional inspection. When a number is not actually used by the design, over-specifying it may create avoidable cost.
Price rule: A BT cost line is reliable only when its material and process assumptions are traceable.
How does layer count and line width affect cost?
Layer count increases lamination time, registration burden, scrap exposure, and inspection work. Fine line/space narrows the supplier pool and may push the build toward substrate-like processes.
For cost control, ask the supplier which requirement is truly expensive. Sometimes moving from an aggressive line width to a slightly wider rule saves more than changing material. Sometimes reducing layer count is impossible because package routing controls the design.
Cost changes usually have a reason inside the process. One quote may assume a stocked material and wider geometry; another may reserve a stricter BT route with more test evidence. The buyer needs that split before awarding on price.
A cost-control note should freeze the assumptions that affect price: material route, geometry, finish, test scope, and delivery date. Any exception can then be priced as a deliberate option.
Decision signal: A cost-down proposal is useful when it shows which assumption changed and what risk stays controlled.
Why does substrate dominate advanced package cost?
In advanced packages, the substrate can become a major cost and yield driver because it connects chip-scale features to board-level assembly. Even when a buyer is not purchasing a CPU package, the same lesson applies: fine substrate rules carry cost through material, process, inspection, and qualification.
BT should therefore be budgeted as an engineered substrate, not a commodity laminate upgrade.
Yield is the hidden multiplier. A design that moves from comfortable PCB geometry into substrate-like features can lose suppliers, slow inspection, and increase scrap risk even if the raw laminate price has not changed much. For budgeting, ask which features are at the supplier’s preferred rule and which are at the quoted minimum. The preferred-rule version often gives a cleaner cost target than the absolute-minimum version.
Cost should be read as a bill of constraints. Material allocation, yield, fine lines, finish, documentation, and delivery pressure can each move price in a different direction.
A useful cost review separates recurring cost from first-build cost. Material allocation, fine geometry, and yield affect every lot, while coupons, documentation, qualification samples, and engineering review may be concentrated in the first order. Mixing those buckets makes a quote look higher or lower than it really is.
Price rule: A BT quote can be compared only after every priced constraint is visible.
How can you reduce BT PCB cost?
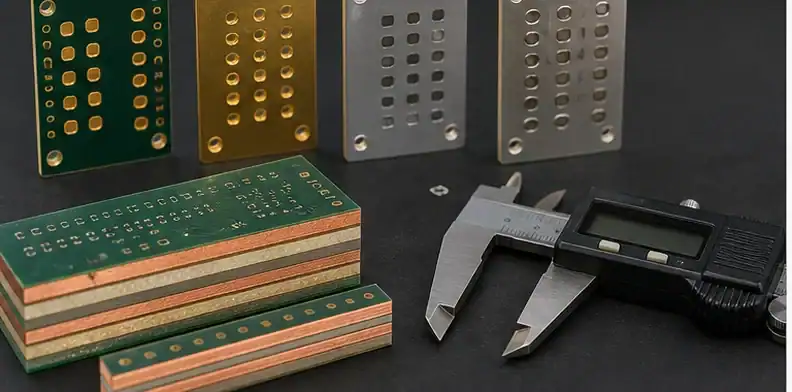
Cost reduction should start with design and evidence, not blind supplier switching. Practical actions include freezing realistic line/space, reducing unnecessary layers, allowing approved equivalent material, optimizing panel use, avoiding unnecessary ENEPIG, and separating prototype evidence from production qualification.
The QueenEMS articles on cutting PCB panel costs and material substitution approval process are useful controls.
The approval boundary should follow the cost driver. Engineering approves changes that affect performance or reliability, purchasing negotiates the commercial option, and quality verifies the evidence promised in the quote.
The risk in cost review is that two quotes can use the same BT label while pricing different material availability, geometry, testing, or delivery assumptions. A cost reduction is safe only after the affected constraint is named and accepted.
Engineering should identify the non-negotiable cost drivers, purchasing should compare like-for-like quotes, quality should confirm which records are required for shipment, and the supplier should separate one-time setup items from recurring lot costs.
Approval rule: Do not accept a lower-cost BT route until the affected cost driver and reliability impact are recorded.
Will BT prices keep climbing?
The safer answer is that BT pricing will remain sensitive to upstream resin, glass cloth, substrate capacity, and AI package demand. Buyers should not assume either continuous inflation or quick normalization.
Use the companion article on the BT supply chain outlook before committing a production schedule. Confirm actual price and lead time with the supplier at RFQ and PO release.
A suspicious cost-down offer hides the trade-off. The lower number may come from stocked material, relaxed geometry, simpler finish, fewer records, or a longer lead time. Ask which assumption changed before approving savings.
Before approving savings, request a cost-driver breakdown and the exact assumptions behind the lower offer. The exception list should show what the buyer is giving up, if anything.
Risk check: Pause cost-down approval when the cheaper quote removes a test, finish, material, or delivery assumption.
Bottom line: budgeting a BT project
Budget a BT project by separating material, structure, finish, evidence, and supply risk. Then decide which requirements can change and which cannot.
Release rule: Do not approve a cheaper quote until engineering confirms the alternate material and process preserve the required package, electrical, moisture, and reliability behavior.
The cleanest cost discussion asks the supplier to show what stays fixed and what can move. Keep the material family, stackup, finish, reliability tests, and approved substitutions fixed while reviewing panel use, order quantity, tooling reuse, and delivery timing. If the supplier wants to reduce cost by changing dielectric thickness, copper, finish, or laminate route, treat that as an engineering change. This makes the cost reduction visible instead of burying it inside a revised quotation.
BT cost is easiest to manage when the buyer separates first-build spending from recurring unit price. First builds may carry extra engineering review, panel planning, material confirmation, drill/process setup, and yield learning. Repeat builds care more about laminate availability, panel utilization, copper balance, inspection flow, and whether the design can run without repeated engineering holds.
Several technical features raise cost because they consume process margin. Narrow traces and spaces reduce yield tolerance. Small vias and filled via-in-pad add drilling, plating, filling, planarization, and inspection steps. Thin dielectrics increase registration sensitivity. Tight impedance requirements can add coupons, test time, and stackup negotiation. Surface finish selection matters too: ENIG, ENEPIG, or package-oriented finishes may be needed for solderability or wire-bond compatibility, but they are not free upgrades.
Material price is only one row in the calculation. A more expensive laminate can still be economical if it improves yield or avoids a package reliability problem. A cheaper alternate can become expensive if it forces another DFM cycle, creates soldering risk, or delays the first qualified build.
Budget control usually starts with three design checks: remove unnecessary tight geometry, avoid over-specifying package-substrate requirements for a board-level job, and confirm whether the same BT family must be frozen for qualification. Those checks do more than push the supplier for a lower number; they clarify which cost is technical necessity and which cost is negotiable preference.
A fair quote comparison also separates engineering-time items from purchase-price items. Tooling, CAM review, impedance coupon setup, material confirmation, and first-article inspection may appear once, while laminate premium, finish choice, yield allowance, and electrical test appear on every lot. Mixing those categories makes a pilot build look artificially expensive or makes a production quote look cheaper than the first qualified order will actually be.
Volume also changes which cost matters most. In a five-piece build, review time, material procurement, and setup can dominate. In repeat production, panel yield, reserved laminate, inspection scope, and stable routing assumptions carry more weight. A useful budget model keeps prototype cost and repeat-lot cost in separate columns.
FAQ
Why is BT expensive?
BT costs more because material, process control, fine features, surface finish, and qualification requirements are more demanding than standard FR-4.
Did BT prices go up in 2026?
Market reports describe price pressure in 2026, but exact values must be confirmed by supplier quote, contract, and material family.
How can I reduce BT cost?
Optimize line/space, layer count, panelization, finish, and approved alternates. Do not remove requirements silently.
Is BT more expensive than FR-4?
Yes, normally. The premium is justified only when BT solves a real reliability, moisture, package, or dimensional need.
Send QueenEMS a BT cost review package
For a BT budget review, share Gerbers or ODB++, stackup, material callout, line/space, layer count, surface finish, panel constraints, quantity breaks, delivery target, and the records required for acceptance through QueenEMS contact. QueenEMS can compare BT substrate cost review cost drivers without quietly changing the approved construction.
Sources
Written by the QueenEMS Engineering Team
Upload your files today · Free DFM check before production · Ship worldwide
Get your PCB prototypes in as fast as 24 hours. We handle FR4, Rogers, and Flex up to 60 layers — free prototypes for 2–4 layer boards, no minimum order.
Just upload your Gerber + BOM — we source every part, assemble, and inspect (AOI + X‑Ray) so you don't have to chase suppliers. Boards ship in as fast as 24 hours.